Pain Points & Technical Challenges
When a precision bearing outer ring is pressed into a housing, a conventional hydraulic press uses only pressure-switch upper and lower limits and cannot identify the four physical stages of the process: force ramp-up, interference engagement, elastic deformation, and yielding. If bearing outside diameter is 3 ?m oversize, force rises sharply. Hydraulic-fluid compressibility delays displacement feedback by 80 ms, causing excessive pressure and travel and creating microcracks in the bearing raceway that are visible under metallographic inspection.
A thin-wall housing with a wall thickness of 1.2 mm is highly susceptible to buckling during press-fitting. Conventional open-loop control cannot decelerate and unload immediately at the yield point, resulting in a long-term scrap rate of 2.8%?4.2%.
Yiruiju Customized Technical Solutions
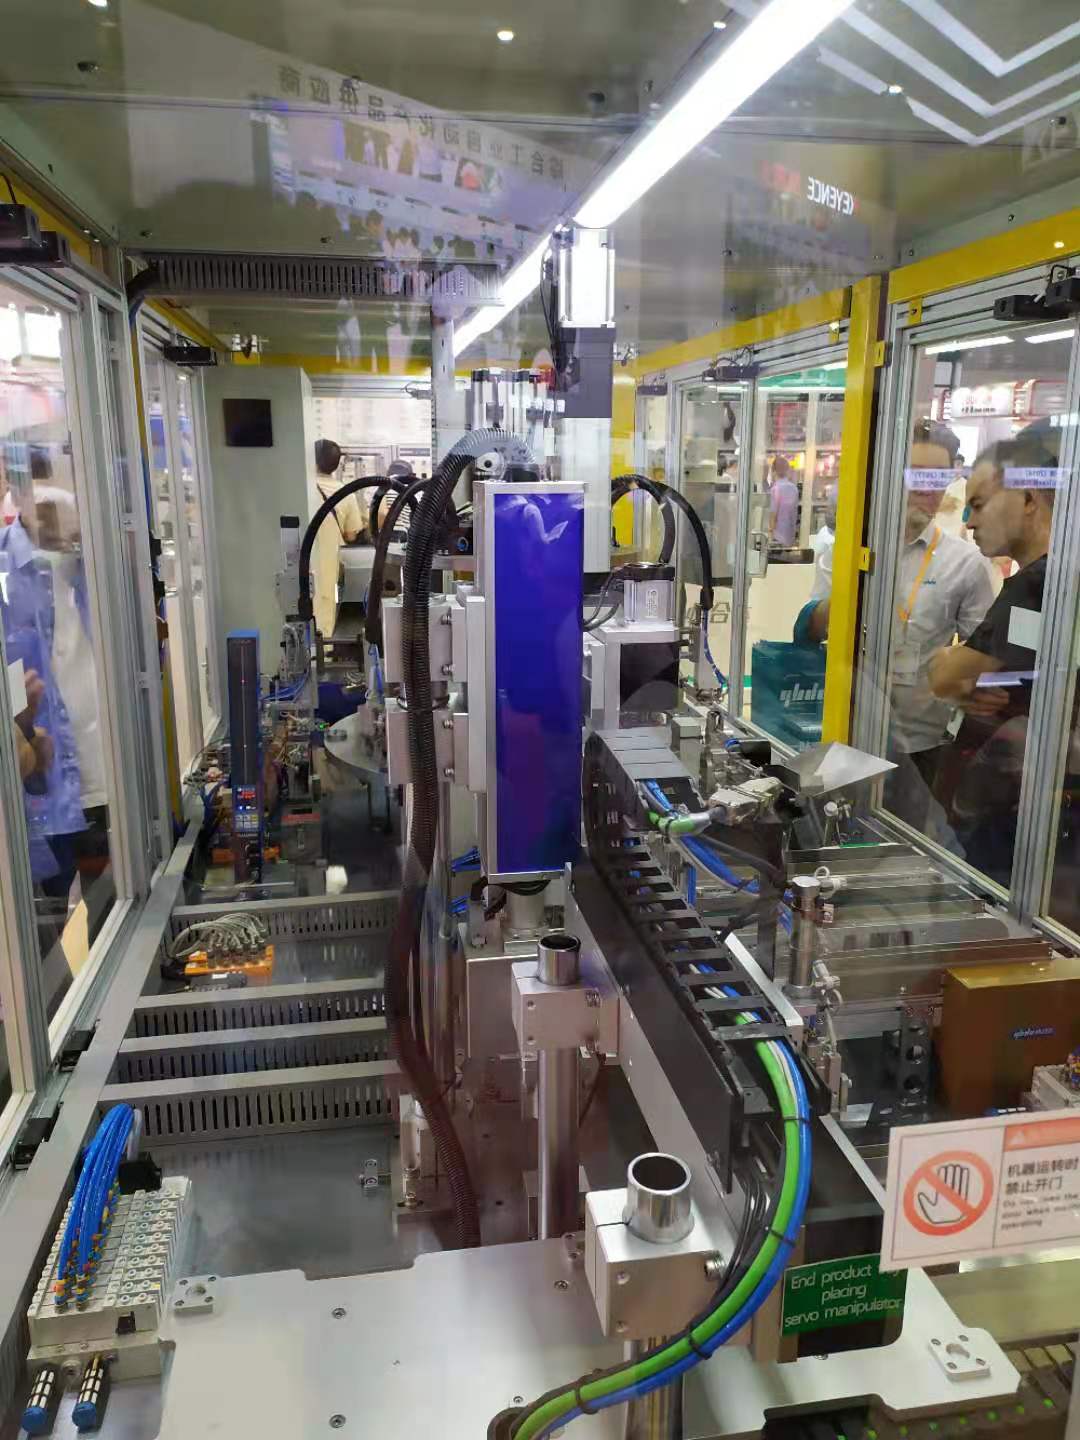
A servo press electric cylinder and a piezoelectric force sensor sampled at 1.5 kHz are combined with real-time slope monitoring of dF/dX. The controller calculates the second derivative of the force-displacement curve. When the dF/dX slope changes beyond a preset threshold, the system locks the current position within 5 ms and reduces speed to a 0.05 mm/s creep rate. The impact peak at interference engagement is avoided and overshoot is held within ?0.008 mm.
A planetary roller screw provides a dynamic load rating equal to 80% of rated static load and reaches 10 million cycles under repeated 20 kN impact. High-accuracy strain-based displacement measurement at the cylinder end directly reports absolute push-rod extension and avoids the ?0.02 mm backlash error caused by torsional deformation when an encoder is located behind the motor.
The controller generates a feature signature for every pressing cycle, including peak force, seating position, and stiffness coefficient K. Dynamic Time Warping compares the signature with a golden curve having Cpk ?1.67, enabling AI-level quality evaluation with a false-judgment rate below 0.05%.