Pain Points & Technical Challenges
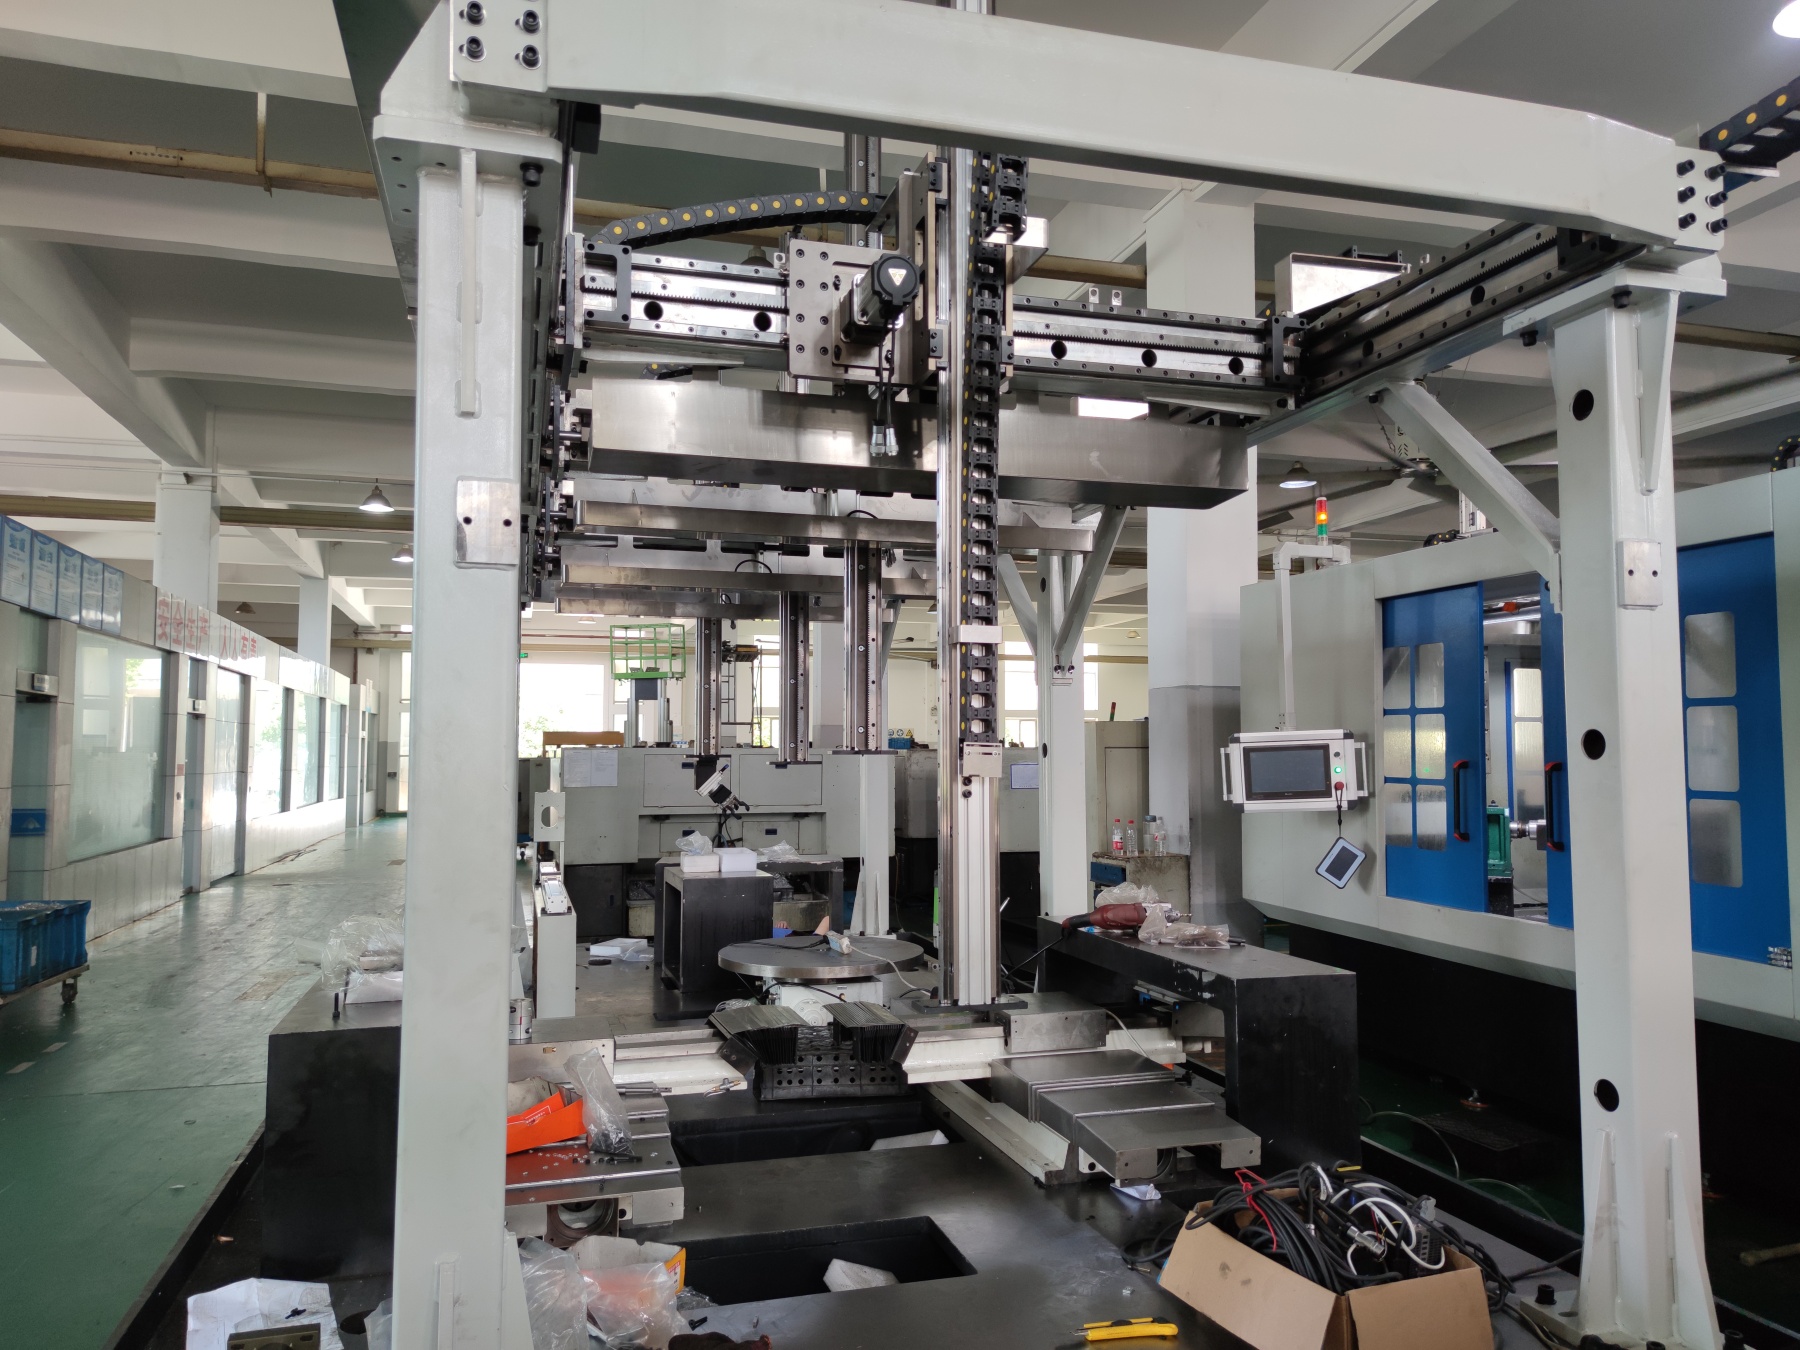
On a large five-face gantry machining center, the Z-axis ram weighs two to three tonnes. As the spindle axis moves with the Y axis, repeated bending of hydraulic lines in the cable carrier causes ?5 bar pressure pulsation in a conventional hydraulic balancing cylinder. During low-speed feed, this creates a periodic nodding error of 0.01?0.02 mm, making it difficult to achieve milled-surface flatness better than 0.015 mm per 1,000 mm.
The spindle tool-clamping mechanism uses disc springs and hydraulic boosting. Continuous hydraulic pressure raises oil temperature by 12?15?C during eight hours of machining. Thermal expansion changes pilot-valve clearance and reduces drawbar force from the nominal 18 kN to 16.2 kN. Fretting at the toolholder taper increases during high-speed milling and shortens toolholder life by 30%.
Yiruiju Customized Technical Solutions
A custom high-thrust, low-backlash servo electric cylinder replaces hydraulic balancing. Dual absolute encoders at the motor and screw provide fully closed-loop control, reducing torsional backlash to no more than 1 arcmin. Thrust fluctuation is below ?0.5% FS and response bandwidth reaches 200 Hz, enabling active reverse compensation for off-center load torque. Full-stroke ram positioning remains within ?0.002 mm in accordance with VDI/DGQ 3441.
The tool-clamping mechanism uses fail-safe disc-spring clamping and electric-cylinder release. At power-on, the cylinder outputs 2.5 times rated thrust to overcome the spring force within 25 ms. Synchronization with the spindle-speed signal reduces a single retract operation during peck drilling from 0.8 seconds to 0.35 seconds.
Eliminating the hydraulic station reduces oil mist near the spindle bearings below 0.1 mg/m? and extends cutting-fluid life from three to eight months. Cylinder design life is at least 20 million cycles, extending spindle-maintenance intervals from three months to 24 months.